What Are the Top 10 Sludge Transfer Pumps for Global Buyers?
Selecting the right sludge transfer pump is becoming a practical priority for wastewater operators, contractors, and industrial buyers. The pressure is measurable. WHO and UNICEF’s Joint Monitoring Programme reported that 3.5 billion people lacked safely managed sanitation services in 2022. More sanitation capacity also means more sludge requiring controlled, reliable movement.
This guide examines ten pump types and configurations used by global buyers. It considers positive displacement pumps, progressive cavity pumps, centrifugal pumps, air-operated diaphragm pumps, and submersible designs. Each option is assessed against solids handling, viscosity, dry-running risk, wear resistance, energy use, maintenance access, and lifecycle cost. The Hydraulic Institute’s pump standards provide useful technical principles for performance testing and selection. The U.S. Environmental Protection Agency also emphasizes energy efficiency and operational reliability when evaluating wastewater equipment.
Real conditions matter. A thickened sludge line may contain rags, grit, sand, or abrasive mineral particles. A pump that performs well with thin primary sludge may struggle beside a dewatering press. That difference is easy to underestimate. Flow rate alone is not enough.
The UN World Water Development Report has repeatedly highlighted the need for better wastewater management and resource recovery. Therefore, global buyers should compare more than catalog capacity. Materials, seal design, control systems, local service, spare-part availability, and documented field experience deserve equal attention. No ranking is perfect. Pump selection still depends on tested sludge data, pipeline geometry, temperature, and operating hours. This introduction frames the comparison, helping readers identify the most suitable sludge transfer pump for demanding, compliant, and cost-conscious applications.
How Sludge Transfer Pumps Work: Flow, Pressure, Solids, and Duty Cycle
What Are the Top 10 Sludge Transfer Pumps for Global Buyers?
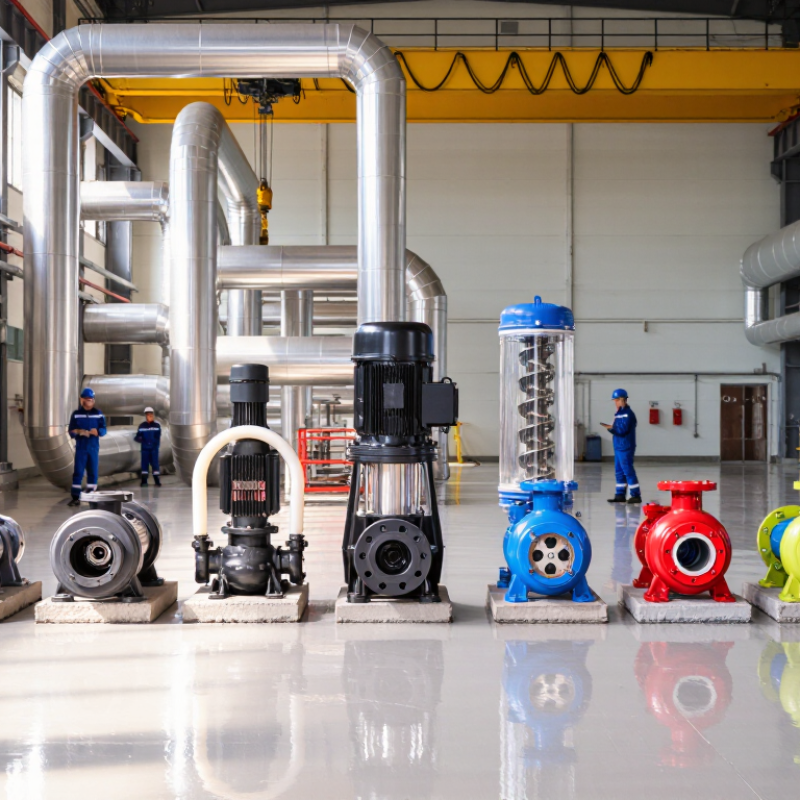
Sludge transfer pumps must move more than water. They handle suspended solids, fibrous matter, grease, and changing moisture levels. Flow rate depends on pipe diameter, solids concentration, and the required transfer distance. Pressure losses rise with long pipelines, narrow bends, valves, and elevation changes. Small details matter.
The U.S. EPA’s 2022 Clean Watersheds Needs Survey estimated over $630 billion in national wastewater and stormwater infrastructure needs. This figure highlights the importance of reliable pumping equipment. For sludge service, buyers should compare actual flow, discharge pressure, solids percentage, and duty cycle. A pump rated for 100 cubic meters per hour may struggle at higher solids content. It may also overheat during continuous operation. Pump curves should be checked against real operating conditions, not only catalog figures.
Tips: Request a solids analysis before selection. Confirm particle size and viscosity. Check whether the pump supports intermittent or continuous duty. Ask for abrasion-resistant wetted parts and accessible inspection points. The Water Environment Federation commonly references sludge concentrations ranging from dilute liquid sludge to much thicker dewatered material. This range changes pump behavior sharply. In my experience, a clean-water calculation can look convincing but fail in the field. I would allow operating margin, yet avoid excessive oversizing. Oversizing can increase energy use, shear, and maintenance costs. Capture pressure readings after installation and review them during seasonal changes.
What Are the Top 10 Sludge Transfer Pumps for Global Buyers?
How sludge transfer pumps work depends on flow rate, discharge pressure, solids size, viscosity, and duty cycle. The chart compares representative operating points for ten commonly used sludge-transfer pump configurations.
How to read the chart: Flow values are representative nominal capacities in cubic metres per hour, while solids-passage values show typical maximum free-passage diameter in millimetres. Actual performance varies with sludge concentration, viscosity, pipe length, elevation, temperature, and operating cycle.
How Buyers Should Compare 10 Pump Options Using ISO 9906 Test Criteria
When global buyers compare the top ten sludge transfer pumps, ISO 9906 should guide the test discussion. The standard evaluates hydraulic performance under controlled conditions. It helps buyers compare flow rate, head, efficiency, and shaft power fairly.
Request test data at the actual duty point, not only the best efficiency point. Check the stated speed, impeller diameter, liquid temperature, and test fluid. Compare pumps tested under the same ISO 9906 acceptance grade.
Grade 1 generally demands tighter tolerances than Grades 2 and 3. The report should also show calibrated instruments, measurement uncertainty, and test repeatability. Small gaps matter when a pump runs continuously.
Look beyond the curve.
Sludge may contain grit, fibers, trapped air, or changing solids concentration. ISO 9906 testing normally uses a controlled liquid, so water performance cannot fully predict field behavior. Ask for solids-handling data, NPSH3 results, wear allowances, and motor loading at start-up.
A clean laboratory curve can still mislead. I have seen buyers focus on peak efficiency while overlooking blocked passages and unstable suction conditions. That is an imperfect comparison, but a useful warning.
A witnessed test can expose vibration, leakage, or unexpected power demand before shipment. Require the same test basis for all ten options, then record every deviation rather than hiding it in a polished spreadsheet.
Progressive Cavity and Rotary Lobe Pumps: Selection Under API 676
What Are the Top 10 Sludge Transfer Pumps for Global Buyers?
Progressive Cavity and Rotary Lobe Pumps: Selection Under API 676
A ten-pump shortlist should compare duty, not marketing language. Progressive cavity and rotary lobe pumps often suit sludge transfer, but they behave differently. Progressive cavity designs provide steady flow at low speed. They handle thick sludge and moderate solids well. Rotary lobe pumps offer easier access and reversible operation. Their wider passages can reduce blockage risks.
API 676 provides a useful framework for rotary positive displacement pump design. Buyers should review pressure ratings, shaft sealing, relief protection, materials, and testing requirements. Do not treat compliance as a simple certificate. The purchase specification must define flow, discharge pressure, temperature, solids size, and expected operating hours. These details decide whether the pump survives daily service.
Field experience changes the ranking. A pump that performs well with activated sludge may struggle with dewatered cake. Elastomer compatibility matters when cleaning chemicals enter the line. Dry-running protection is essential for progressive cavity pumps. Rotary lobe units also need careful speed control and adequate suction conditions. Keep the suction pipe short and avoid sharp bends. Simple choices matter.
A perfect ranking does not exist. I would not trust a laboratory result alone. Request a witnessed performance test using representative sludge when possible. Also inspect wear parts after trial operation. Maintenance access, spare-part availability, and operator skill can outweigh a small efficiency advantage. A technically strong selection can still fail when the installation is rushed.
Centrifugal, Diaphragm, and Peristaltic Pumps: Match Type to Sludge
Centrifugal, diaphragm, and peristaltic pumps handle sludge in different ways. The right choice depends on solids, viscosity, flow needs, and maintenance access—not just a supplier’s headline capacity. A pump that performs well with thin, screened sludge may struggle when stringy fibers or grit enter the line.
Centrifugal pumps suit relatively fluid sludge and steady, higher-volume transfer. Check the impeller passage and wear materials against the largest expected particles; abrasive grit can quickly change clearances. They need reliable priming and can lose efficiency as the mixture thickens. Good for consistent flow. Not every sludge is consistent.
Diaphragm pumps move sludge through a chamber using a flexible diaphragm, making them useful for variable feed and intermittent duty. Their pulsing flow may require a dampener where smooth delivery matters. Peristaltic pumps squeeze a hose or tube, keeping the sludge contained within it. This can simplify cleanup and help with shear-sensitive mixtures, though hose wear and replacement intervals deserve close attention. Inspect samples, measure solids content, and ask operators how often the feed changes. Those details can outweigh a neat specification sheet. A short site trial is sensible; it may still miss seasonal variation.
How to Rank 10 Pumps by Capacity, Solids Handling, Efficiency, and Cost
A useful top-ten sludge pump ranking should begin with the duty point, not the catalogue headline. Record flow, total dynamic head, operating hours, and the largest expected solids. Then compare each pump’s tested capacity at that duty point; maximum flow alone can mislead. The U.S. Department of Energy’s Improving Pumping System Performance guide emphasizes evaluating the whole pumping system, including operating conditions and energy use. That matters: a pump that moves 100 cubic metres per hour in a clean-water test may struggle with thick sludge or fibrous debris. Check passage size, impeller design, and whether the unit can handle intermittent feed. Ask for test curves. Do not assume.
Efficiency deserves a measured comparison. The International Energy Agency’s energy-efficiency work on electric motor-driven systems identifies pumps as a major motor-system application, making operating hours and power draw important lifecycle costs. For each candidate, estimate annual energy from measured input power, rather than relying on a broad efficiency claim. Include wear parts, maintenance access, and expected replacement intervals in the cost score. A lower purchase price can become expensive when abrasive solids wear the casing or seals. These estimates are imperfect. Sludge varies by site, and published data may not match actual service. Rank the ten options using consistent weights for capacity, solids handling, efficiency, and lifecycle cost; document assumptions so buyers can challenge them.
What Are the Top 10 Sludge Transfer Pumps for Global Buyers? — How to Rank 10 Pumps by Capacity, Solids Handling, Efficiency, and Cost
Indicative comparison of common pump types for sludge transfer. Performance and purchase costs vary with sludge properties, materials, motor, controls, duty point, and region; confirm figures with suppliers for the actual application.
| Rank |
Pump type |
Typical capacity |
Solids handling |
Typical hydraulic efficiency |
Indicative equipment cost (USD) |
Best-fit application / trade-off |
| 1 |
Progressive cavity |
Approx. 0.5–500 m³/h |
Handles viscous sludge and moderate soft solids; passage depends on rotor/stator design. |
Approx. 50–75% |
$2,000–$40,000+ |
Strong all-round choice for metered, low-pulsation transfer; stator wear and dry-running sensitivity require attention. |
| 2 |
Rotary lobe |
Approx. 1–400 m³/h |
Good for soft, fibrous solids; allowable particle size depends on lobe geometry and clearances. |
Approx. 50–75% |
$5,000–$60,000+ |
Reversible and serviceable with convenient access; can be sensitive to abrasive grit and hard debris. |
| 3 |
Peristaltic (hose) pump |
Approx. 0.1–100 m³/h |
Handles abrasive, corrosive, and shear-sensitive slurries; solids are limited by hose bore and particle size. |
Approx. 30–60% |
$3,000–$50,000+ |
No seals or valves in contact with the pumped fluid; hose replacement is a recurring cost. |
| 4 |
Recessed-impeller centrifugal |
Approx. 5–1,500 m³/h |
Suitable for stringy or solids-bearing liquids; passage varies substantially by casing and impeller. |
Approx. 40–70% |
$2,000–$35,000+ |
Simple, relatively high-flow option for low-to-medium viscosity sludge; not ideal for very thick sludge. |
| 5 |
Vortex centrifugal |
Approx. 5–1,000 m³/h |
Passes large, soft solids with reduced impeller contact; exact passage is model-specific. |
Approx. 25–55% |
$1,500–$25,000+ |
Clog-resistant choice for dilute sludge and debris; lower efficiency can increase energy costs. |
| 6 |
Twin-screw |
Approx. 1–1,000 m³/h |
Can transfer viscous fluids and solids-bearing sludge; allowable solids depend on screw pitch and clearances. |
Approx. 55–80% |
$15,000–$150,000+ |
Broad operating range and relatively smooth flow; typically higher initial cost and more complex maintenance. |
| 7 |
Submersible solids-handling centrifugal |
Approx. 5–1,500 m³/h |
Designed for wastewater solids; passage size and rag-handling capability vary by impeller design. |
Approx. 45–75% |
$1,000–$30,000+ |
Convenient for wet wells and sumps; access for inspection and lifting arrangements should be considered. |
| 8 |
Air-operated double-diaphragm |
Approx. 0.1–60 m³/h |
Can handle solids and abrasive fluids; ball-valve passage and diaphragm material are key limits. |
Low overall system efficiency; depends on compressed-air supply. |
$500–$15,000+ |
Portable and self-priming with no electric motor at the pump; compressed-air use can be costly. |
| 9 |
Progressive screw (Archimedean) |
Approx. 10–5,000 m³/h |
Handles screened or unscreened wastewater with solids, depending on channel design and installation. |
Approx. 60–80% near design conditions |
$20,000–$500,000+ |
Efficient for large flows at low head in open channels; requires substantial civil works and space. |
| 10 |
Piston / ram pump |
Approx. 0.1–100 m³/h |
Can move thick sludge and large solids through suitable valves and passages; application-specific design is essential. |
Approx. 50–80% |
$10,000–$200,000+ |
Useful for very high-solids or dewatered sludge and long-distance transfer; pulsed flow and high capital cost are common considerations. |
How to use this ranking: It is a general screening order balancing versatility, solids handling, efficiency, and cost—not a universal performance guarantee. Verify flow, total dynamic head, solids concentration and size, viscosity, abrasiveness, suction conditions, materials, and maintenance requirements before selection. Cost figures are broad budgetary ranges for pump equipment only, not installed-system quotations.